Buzz Saw Blade Types: How to Pick the Right One for Wood, Metal & Masonry
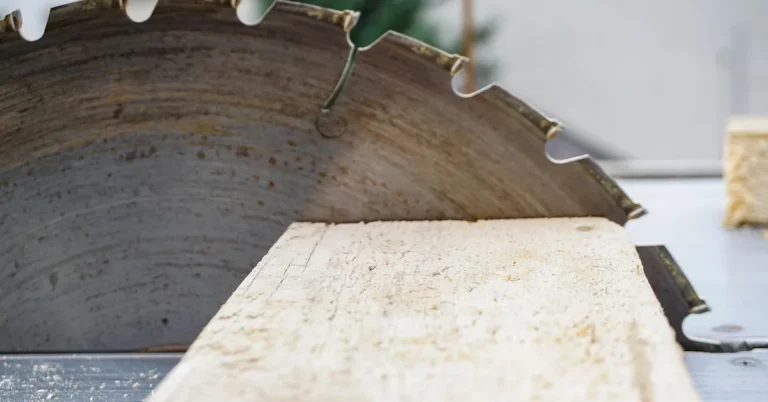
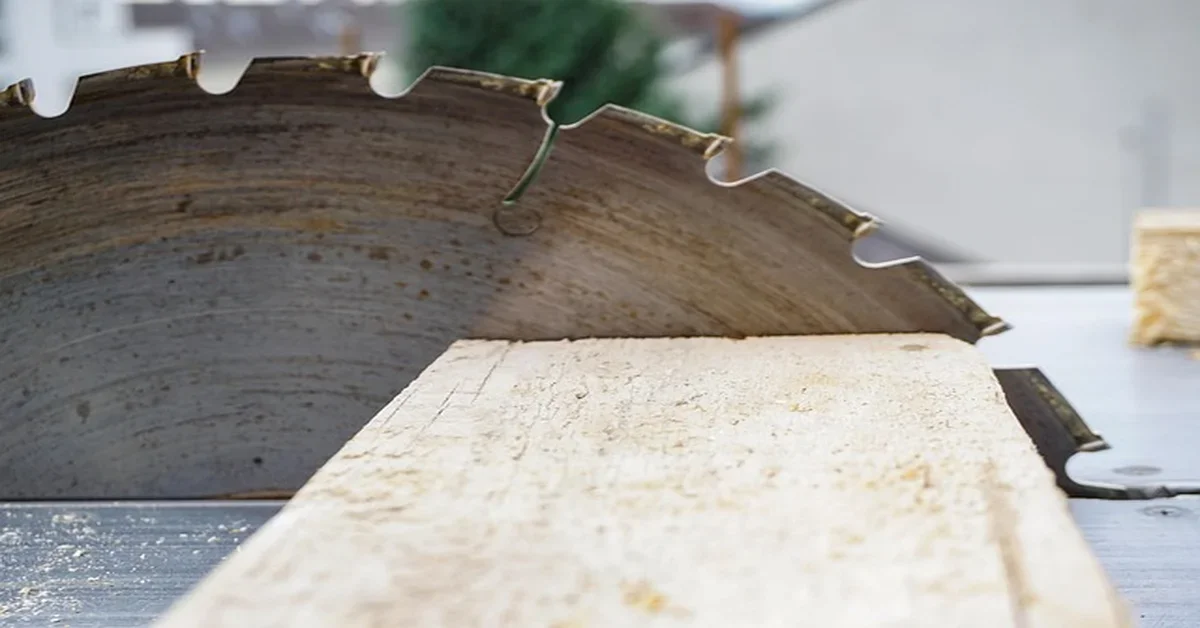
A “buzz saw blade” isn’t a specific product – it’s the everyday name for any circular saw blade, earned from the buzzing whine carbide teeth make at full RPM. That casual name hides a real engineering choice underneath it: tooth count, grind pattern, plate thickness, and bore size all change what a given blade is actually good at cutting. Grab the wrong one and you don’t just get a rougher edge – you can burn softwood, chip out plywood veneer, or overheat a thin-kerf plate that was never designed for the cut you’re asking it to make.
What Actually Separates One Buzz Saw Blade From Another
Every circular saw blade is defined by four specs, and all four matter more than the brand name stamped on the plate. Diameter has to match your saw – 7-1/4 inch is standard for full-size circular saws, 6-1/2 inch for compact/cordless models, and 10 inch for most table saws. Arbor (bore) size is almost always 5/8 inch on US circular saw blades, though some table saw and metric blades use 20mm or 1 inch – mounting a blade on the wrong arbor with a bushing is a real safety issue, not a minor inconvenience. Kerf is the width of the slot the blade cuts; thin-kerf blades remove less material and let underpowered saws cut faster, but they also flex more and are more prone to wandering in a long rip. Max RPM rating is stamped on the plate for a reason – running a blade above its rating is how plates crack or delaminate.
Best All-Purpose Finish Blade
 |
Diablo Finish Saw Blade, 7-1/4″ 40T – $20.15 A 40-tooth ATB carbide blade sized for standard 7-1/4″ circular saws – the tooth count this guide recommends for smooth crosscuts and general finish work.
|
Buzz Saw Blade Types By Tooth Grind
The grind ground into each tooth – not the tooth count alone – is what actually determines what a blade cuts well. Four grinds cover almost every circular saw blade you’ll ever buy:
- Alternate Top Bevel (ATB): teeth alternate left and right bevel angles, which shears wood fibers cleanly across the grain. This is the standard grind for crosscut and finish blades.
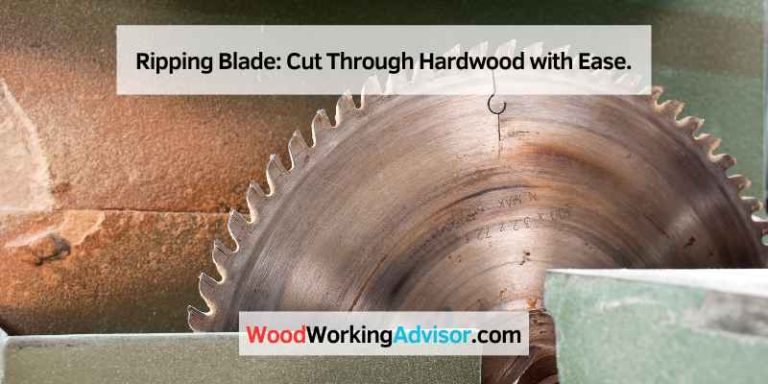
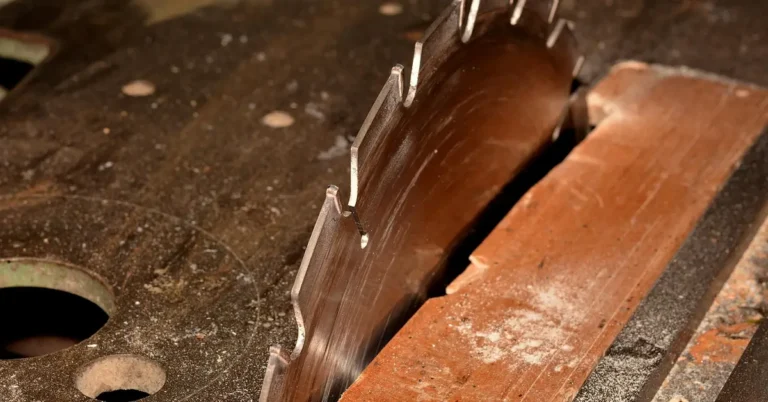
- Flat Top Grind (FTG): teeth are flat-topped and chisel-like, built to chop through wood fibers along the grain fast. Rip blades use this grind, and they intentionally carry far fewer teeth than a crosscut blade.
- Combination Grind: groups of four or five ATB teeth separated by one larger FTG-style raker tooth and a deep gullet, giving one blade that can rip and crosscut reasonably well without a blade change.
- Triple Chip Grind (TCG): alternates a flat tooth with a trapezoid-shaped tooth that has its corners chamfered off. It resists chipping on abrasive or brittle material, which is why it shows up on blades rated for non-ferrous metal, plastic laminate, and MDF.
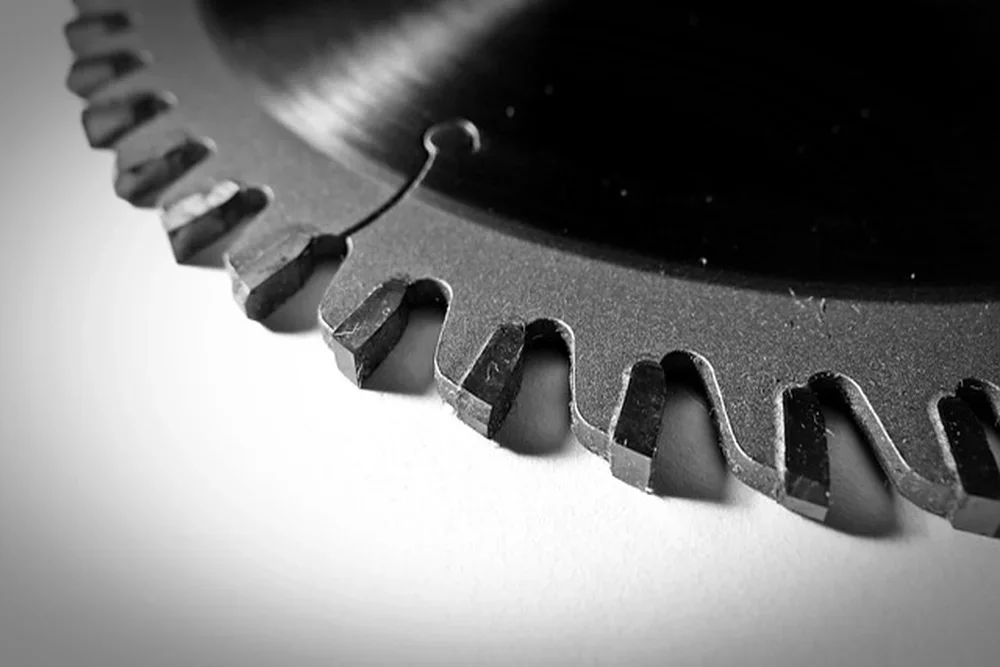
A common assumption is that more teeth always means a better blade. That’s only true for finish quality, not for every cut. A 60-tooth blade leaves a smoother edge than a 24-tooth blade because each tooth removes a smaller bite of material – but on a rip cut, that same high tooth count is a liability. Ripping removes a lot more material per pass than crosscutting, and a high-tooth-count blade has smaller gullets between teeth with less room to clear that sawdust. The chips pack into the gullets, friction spikes, and the blade overheats and can burn the wood or bind in the cut. That’s exactly why dedicated rip blades intentionally use as few as 24 teeth on the same 7-1/4 inch plate that a finish blade carries 40 to 60 teeth on – fewer, larger teeth with bigger gullets move more waste per rotation and keep the blade running cooler.
Matching Blade Material To What You’re Cutting
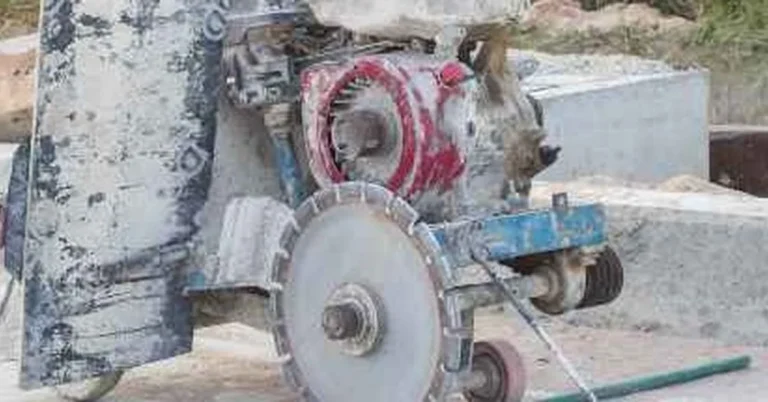
The plate and teeth material matters as much as the grind. High-speed steel (HSS) blades are the cheapest option and can be resharpened at home with a file, but they dull quickly against hardwood and plywood glue lines – they’re realistically only worth buying for occasional softwood cuts. Carbide-tipped blades are the standard for nearly everything else: tungsten carbide teeth brazed onto a steel plate hold an edge roughly 10 to 20 times longer than HSS against the same material, which is why carbide dominates both budget and premium blades sold today. Diamond blades aren’t really “saw teeth” at all – they use a diamond-impregnated metal rim (continuous rim for clean tile cuts, segmented rim for faster masonry and concrete cutting) and are the only real option once you’re cutting stone, brick, or cured concrete rather than wood or metal.
Cutting metal changes the equation again. Thin sheet steel and aluminum call for carbide or TCG-ground blades specifically rated for metal, run at a much lower feed rate than wood – forcing a wood-rated blade through metal overheats the teeth and can shatter carbide tips. Abrasive cut-off wheels (not toothed blades at all) are a separate category still commonly grouped under “buzz saw blade” searches, and they’re the better choice for thick or hardened steel where a toothed carbide blade would wear out in minutes.
Buzz Saw Blade Uses In The Shop And On The Job Site
In woodworking, buzz saw blades handle everything from rough framing lumber to finish trim – the difference is almost entirely the tooth grind and count discussed above, not a different category of blade. In metal fabrication, carbide and TCG blades cut thin ferrous and non-ferrous stock without the sparks and heat of an abrasive wheel, which matters in a shop where fire risk or warping thin metal is a concern. On construction and demolition sites, diamond blades and heavy 24-tooth carbide rip blades see the most use – cutting through masonry, old framing lumber that may have embedded nails, and rough-sawn material where finish quality is irrelevant and cutting speed is what matters.
If you’re building out a broader blade collection for a table saw or miter saw, it’s also worth reading how tooth count changes miter saw cut quality specifically – the same rip-vs-finish tradeoff above applies there too, just at higher tooth counts because miter saws are almost never used for ripping.
Maintaining A Buzz Saw Blade So It Actually Lasts
One piece of advice that gets repeated online for circular saw blades is wrong: you cannot “tension” a buzz saw blade the way you would a bandsaw blade. A circular blade is a rigid disk, not a flexible band running between two wheels, so there’s no tension adjustment to make – if a circular blade is warped or has runout, the fix is replacement, not tensioning. What actually extends a buzz saw blade’s life is simpler: clean pitch and resin off the plate and gullets with a dedicated blade cleaner or diluted citrus degreaser (harsh solvents can attack the brazing that holds carbide teeth on), dry it fully before storing to prevent rust on the steel plate, and check it against a flat surface periodically for warping. A blade that’s merely dull but still flat can usually be professionally resharpened two or three times before the carbide is too thin to grind again – a blade that’s warped, has a missing tooth, or shows a hairline crack near the gullet should be retired immediately regardless of how sharp the remaining teeth look.
Safety Practices When Running A Buzz Saw Blade
Most buzz saw blade injuries trace back to kickback, not the blade itself failing. On a table saw, keep the riving knife or splitter installed – it stops the kerf from pinching closed behind the blade and throwing the workpiece back at you, which is the single biggest kickback cause. On any saw, let the blade reach full speed before it contacts the material, feed at a steady pace instead of forcing it, and never remove a blade guard to “see the cut better.” Eye protection and hearing protection aren’t optional extras – carbide teeth running at 8,000+ RPM throw debris fast enough to cause permanent eye injury, and the noise level from a blade that size is loud enough to cause hearing damage with repeated daily exposure.
Frequently Asked Questions For Buzz Saw Blade
What Is A Buzz Saw Blade Used For?
A buzz saw blade is the everyday term for a circular saw blade, used to cut wood, metal, or masonry depending on the tooth grind and material the specific blade is built for. The same term covers rip blades, crosscut blades, combination blades, and diamond blades – the right one depends entirely on the material and type of cut.
What’s The Difference Between A Rip Blade And A Crosscut Blade?
A rip blade uses a flat-top grind with a low tooth count, usually 24 teeth on a 7-1/4 inch plate, and cuts fast along the wood grain with large gullets that clear waste quickly. A crosscut or finish blade uses an alternate top bevel grind with a much higher tooth count, typically 40 to 60 teeth, which shears fibers cleanly across the grain for a smooth edge but would overheat if used to rip.
Can I Use A Buzz Saw Blade To Cut Metal?
Only if the blade is specifically rated for metal – typically a carbide or triple chip grind (TCG) blade designed for thin ferrous or non-ferrous stock, run at a slower feed rate than wood. A standard wood-rated blade will overheat and can shatter its carbide teeth if forced through metal.
How Do I Know When To Replace A Buzz Saw Blade?
Replace it when it’s warped, has a missing or chipped tooth, shows a crack near the gullet, or has already been resharpened two to three times and no longer holds an edge. A dull but otherwise flat, undamaged carbide blade can usually be professionally resharpened rather than replaced outright.
Conclusion
“Buzz saw blade” is a catch-all name, but the blade underneath it isn’t one-size-fits-all. Match the tooth grind to the cut – flat-top for ripping, alternate top bevel for crosscutting, triple chip for abrasive or non-ferrous material, diamond for masonry – and match the plate material to what you’re actually cutting rather than reaching for whatever blade is already mounted. Do that, and a buzz saw blade will run cooler, last longer, and leave a cleaner cut than one picked by tooth count alone.
Sponsored / affiliate links. As an Amazon Associate I earn from qualifying purchases. I may earn additional commission from eligible campaigns.