Reciprocating Saw for Metal: Blade TPI and Cutting Guide
Cutting metal with a reciprocating saw comes down to three things a lot of guides skip: the right TPI (14-18 for most jobs), a bi-metal blade instead of a wood blade, and turning orbital action off. Get those wrong and you’ll snap blades, throw sparks everywhere, or stall the cut halfway through a pipe. Here’s the blade math, the setup, and the technique that actually works.
What Blade TPI You Actually Need for Metal
Teeth-per-inch (TPI) is the single biggest factor in whether a metal cut goes clean or goes badly. Lower TPI blades have bigger gullets between the teeth, so they clear material fast but leave a rougher edge. Higher TPI blades cut slower and smoother, and they’re the only safe choice on thin stock because coarse teeth catch on thin metal and can grab the saw right out of your hands.
Best 14 TPI Metal-Cutting Blade Set
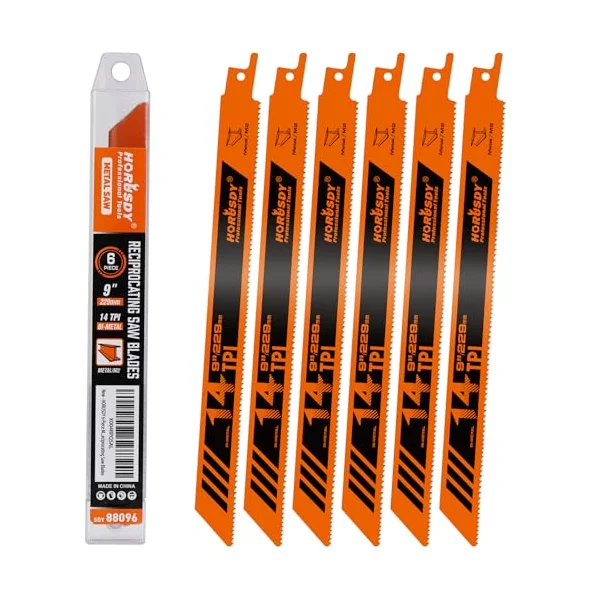 |
HORUSDY 9-Inch 14 TPI Bi-Metal Blades (6-Pack) – $11.39 14 TPI sits right in the general metal-cutting range this guide recommends, so these are the blades to grab before you cut pipe, rebar, or angle iron with your reciprocating saw.
|
- 14-18 TPI: the general-purpose range for conduit, rebar, copper pipe, steel studs, and angle iron
- 18-24 TPI: required for anything under 1/8 inch thick – sheet metal, thin-wall tubing, auto body panels
- 8-10 TPI: reserve for thick or soft scrap metal and demolition-style cuts where speed matters more than a clean edge
Metal type matters too. Aluminum is soft enough to cut with the same 14-18 TPI blade you’d use on mild steel. Stainless steel work-hardens as you cut it, so a higher-TPI blade (20-24) that takes smaller bites per stroke will last longer and won’t glaze over as fast. Cast iron splits the difference at 10-14 TPI.
Bi-Metal vs. Carbide-Tipped Blades
Almost every metal-cutting reciprocating saw blade sold today is bi-metal: high-speed steel (HSS) teeth electron-welded onto a body of tougher, more flexible high-carbon steel (HCS). The HSS teeth hold an edge through repeated flexing, and the HCS spine keeps the blade from snapping when it binds in a cut – which is exactly the failure mode an all-HSS or all-HCS blade doesn’t survive.
Carbide-tipped and carbide-grit blades cost roughly three to five times more, but they’re the right call for hardened steel, cast iron, or stainless where a bi-metal blade would dull within a handful of cuts. For routine work on mild steel pipe, studs, rebar, and angle iron, bi-metal is the better value and the safer default.
Saw Setup: Why Orbital Action Is Wrong for Metal
This is the step most metal-cutting guides get backwards. Orbital action adds a small elliptical motion to the blade’s stroke so it bites more aggressively into wood fiber – great for framing lumber, bad for metal. On steel or aluminum, that same elliptical motion makes the blade wander sideways in the kerf, chews out the teeth faster, and is a leading cause of blade snapping and kickback. Before you cut any metal, flip the saw’s mode selector to straight-line (non-orbital) stroke.
Stroke speed matters just as much. Run the saw at a slower speed setting for metal than you would for wood – a fast stroke generates heat faster than the cut can dissipate it, which is what actually dulls or blues a blade, not the metal itself. Let the blade’s teeth do the cutting; forcing the saw forward just increases friction and heat without cutting any faster.
Step-by-Step: Making a Clean Metal Cut
- Clamp the workpiece. Metal transmits vibration far more than wood, so an unclamped pipe or bar will buzz, walk, and chew up the blade. Use a vise or locking clamps as close to the cut line as you can.
- Install the right blade and confirm it’s seated. Match the TPI to the material using the chart above, and make sure the blade is locked fully into the clamp before starting the saw.
- Switch off orbital action and set the speed dial to a moderate-to-slow setting.
- Start the cut at a shallow angle so only a few teeth engage the metal at first, then level the blade flat once the kerf is established.
- Apply steady, light pressure and let the stroke speed and blade do the work – don’t lean into the saw.
- Back off periodically on thick material to let the blade cool and clear metal shavings from the gullets; a blade packed with swarf stops cutting and starts rubbing.
Safety Measures
Metal cutting throws hot metal shavings and occasional sparks, and a bound or snapped blade can kick the saw back toward you. Treat these as non-negotiable:
- Safety glasses or a full face shield: metal shavings and sparks travel farther and hotter than wood dust
- Gloves rated for cut and heat resistance: freshly cut metal edges are sharp and can still be hot
- Hearing protection: a reciprocating saw against steel is louder than the same saw in wood
- Secure clamping, every time: most kickback incidents trace back to an unclamped or loosely clamped workpiece shifting mid-cut
- Clear the cut path: know what’s on the other side of the material before you cut through it, especially with pipe or studs that may carry wiring
Maintenance and Blade Care
Metal cutting is harder on blades than wood cutting, so check them more often. Inspect the teeth after every job for missing or folded-over teeth, a blade that’s gone blue from overheating (a sign the temper is shot and it will fail early), or visible bowing. Replace it rather than pushing a dull blade through more cuts – a dull blade needs more force, and more force is what causes snapping and kickback.
After metal-cutting sessions, brush metal filings out of the shoe and blade clamp before they work into the mechanism, and add a drop of light machine oil to the blade clamp and orbital selector so they don’t seize from rust. If you also cut wood with the same reciprocating saw blade mount, keep your wood and metal blades in separate slots so you’re not grabbing the wrong TPI mid-job.
For a wider comparison across saw types – circular saw, table saw, and reciprocating saw – including RPM numbers for blade-tip speed, see our guide to picking the right saw blade for cutting metal. If you’re still shopping for the saw itself rather than just blades, our reciprocating saw pricing breakdown covers what separates a budget saw from a pro-grade one.
Frequently Asked Questions
What TPI blade do I need to cut metal with a reciprocating saw?
Use 14 to 18 TPI for general metal work like conduit, rebar, copper pipe, and angle iron. Drop down to 8 to 10 TPI only for thick, soft scrap metal, and go up to 18 to 24 TPI for sheet metal and thin-wall tubing under 1/8 inch, since coarse teeth snag and tear thin stock instead of cutting it.
Should I use orbital action when cutting metal?
No. Orbital action adds a forward-and-back arc to the blade stroke, which is meant to clear wood chips faster. On metal it makes the blade wander off your cut line and dramatically increases the chance of snapping a blade or kicking the saw back. Switch the saw to straight (non-orbital) stroke mode before cutting any metal.
Bi-metal or carbide-tipped blade for metal?
Bi-metal blades (high-speed steel teeth welded to a flexible high-carbon steel body) are the right default for most metal cutting – pipe, studs, rebar, angle iron – because they resist snapping and cost far less. Reach for a carbide-tipped or carbide-grit blade only for hardened steel, cast iron, or stainless, where a bi-metal blade would dull in a few cuts.
Can a reciprocating saw cut through thick steel?
Yes, but slow down. A reciprocating saw can cut steel plate, thick pipe, and rebar, but thick or hardened steel needs a lower stroke speed, steady downward pressure instead of forcing the blade, and a coarser 8-14 TPI blade so the teeth don’t clog with metal shavings and overheat.
Conclusion
A reciprocating saw cuts metal reliably once you match three things: a 14-18 TPI bi-metal blade for most jobs, straight (non-orbital) stroke mode, and a slower speed than you’d use on wood. Clamp the workpiece, let the blade do the cutting, and swap blades before they go dull rather than after they snap.
Sponsored / affiliate links. As an Amazon Associate I earn from qualifying purchases. I may earn additional commission from eligible campaigns.