Can You Router Plywood? Yes – Here’s How to Avoid Tear-Out
Yes, plywood can be routered for edge profiles, dado grooves, and flush trimming – the material itself isn’t the problem. What trips people up is that plywood isn’t solid wood: it’s built from thin veneer layers glued together with the grain running a different direction in each layer, and a bit chosen for solid stock will tear straight through that cross-grain structure. Match the bit type and feed technique to how plywood is actually built, and a router handles it as cleanly as anything else in the shop.
Yes, You Can Router Plywood – Here’s the One Thing That’s Different
A router cuts plywood the same way it cuts solid wood mechanically, but plywood’s alternating veneer layers change which bit and feed direction actually give you a clean edge. Get those two choices wrong and you’ll chip out the exact same panel that a slightly different bit would have cut perfectly.
Best Bit for Plywood Edges
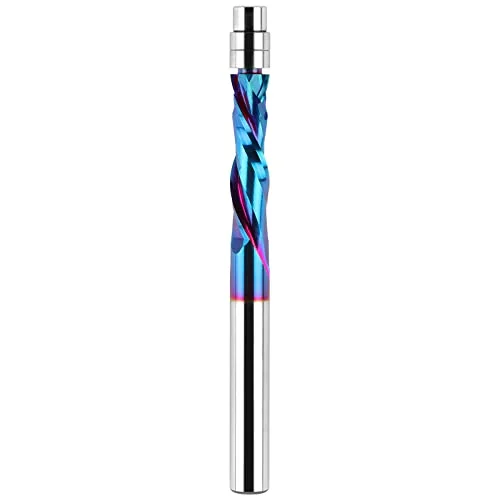 |
EANOSIC Compression Spiral Flush Trim Router Bit – $24.59 A compression bit cuts down into the top face and up into the bottom face at once, which is exactly what keeps both sides of a plywood edge from chipping during dado, trim, or template cuts.
|
Why Plywood Chips and Tears Out More Than Solid Wood
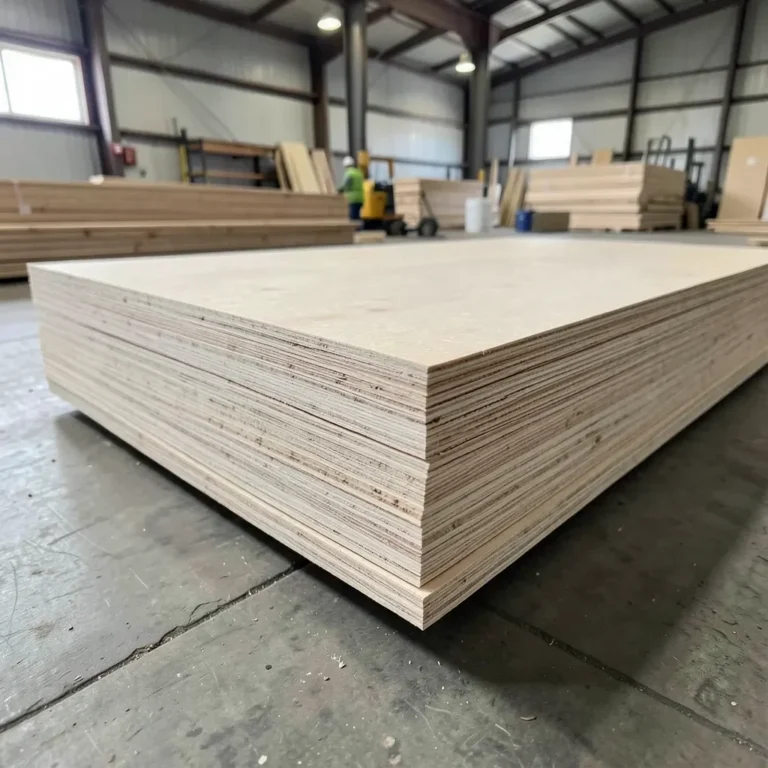
Plywood is built from 3 to 7+ thin veneer layers, each one glued with its grain running roughly perpendicular to the layer below it. That cross-grain structure is what gives plywood its strength and stability, but it’s also exactly why it tears out more than solid wood under a router bit. A round-over or dado cut passes through several of those layers at once, and every layer whose grain runs against the direction the bit is cutting is a chance for the veneer to lift and splinter instead of shearing cleanly.
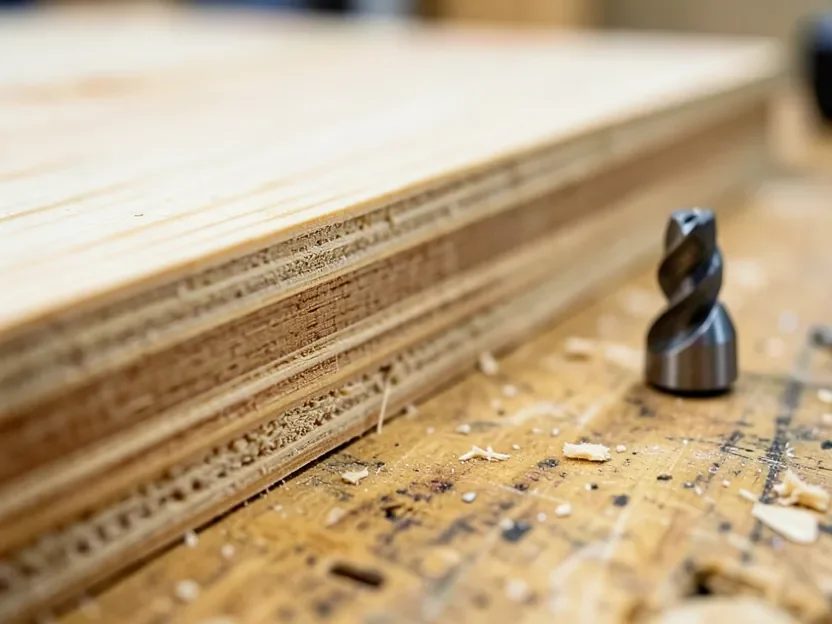
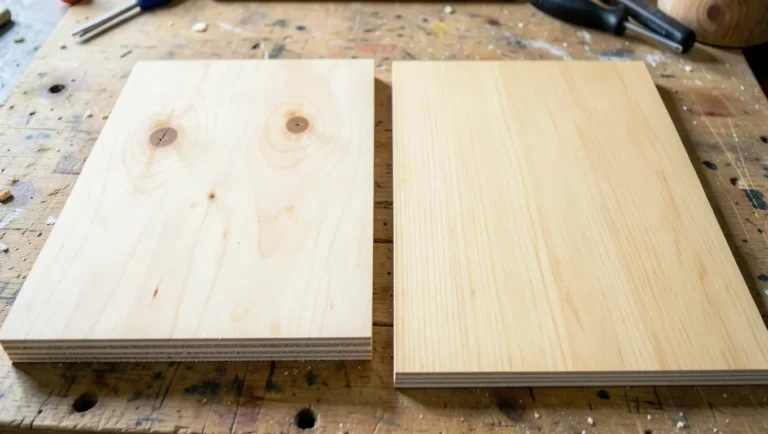
Plywood grade makes this worse or better. Lower grades use thinner, lower-quality face veneer that chips through to the core layer much more easily than the thicker face veneer on a cabinet-grade sheet — worth checking before you start a routing project, since the same bit and technique that leave a clean edge on A-grade face veneer can still chip out on a thinner B or C-grade face.
The “Just Go Against the Grain” Myth
A lot of older advice on routing plywood boils down to “feed against the grain and you’ll be fine.” That’s incomplete, and on a cross-grain material like plywood it’s not really a coherent instruction in the first place — there’s no single grain direction to feed against, since each veneer layer runs a different way. What actually controls tear-out is bit geometry and feed direction relative to the bit’s rotation, not the wood’s grain.
An upcut spiral bit pulls chips upward and out of the cut, which is useful for dust clearance on deep cuts in solid wood, but on plywood it also lifts the top-face veneer as it exits — that’s the single most common cause of a chipped top edge. A downcut spiral bit does the opposite: it presses the fibers down into the panel instead of lifting them, which keeps the top face clean. A compression spiral bit combines both (downcut near the top, upcut near the bottom) so it cleans up both faces of the cut at once, which is why it’s the standard recommendation for flush-trim and template work on plywood and other veneered panels.
Feed direction matters too, separately from bit type. A conventional feed, where the bit rotation cuts into the material as you push the router forward, controls chip-out on the main pass. A climb cut, where you feed in the same direction the bit is spinning, can leave a slightly cleaner finish, but it lets the router pull itself along the cut if you’re not holding it firmly, so it only belongs in a router table’s larger cuts or as a very light, controlled final cleanup pass — never as your main cutting technique on a handheld router.
Cutting Dado Grooves and Slots in Plywood with a Router
A dado (a flat-bottomed groove routed across the panel to seat a shelf or divider) is one of the most common router cuts made in plywood, and it’s also one of the easiest to chip out because the top face stays visible on the finished piece. A downcut spiral bit run against a straightedge or router edge guide gives the cleanest top edge. Take the cut in two or three shallow passes instead of trying to hit full depth in one pass — each lighter pass gives the bit less material to tear at once, and it’s the difference between a crisp groove and a ragged one on thin face veneer.
Before setting bit depth, measure the actual panel with calipers rather than trusting the nominal size on the label. Most “3/4-inch” plywood actually measures closer to 23/32 inch, and a dado cut to a nominal depth on undersized stock leaves a groove that’s too loose for a snug shelf fit. Support the plywood fully underneath the cut line, too — plywood flexes more than solid lumber of the same thickness, and any sag under the router changes your depth of cut mid-pass.
Routing Edge Profiles on Plywood (Round-Overs and Chamfers)
Round-over and chamfer bits work on plywood the same way they do on solid wood, but bit radius matters more here: a bit radius sized for the panel’s thickness keeps the profile from cutting so deep it exposes an awkward number of veneer layers in the curve. On 3/4-inch stock, a 3/8-inch bit run on one face, then flipped and repeated on the other, gives a fuller, more symmetrical round-over than trying to remove the whole radius from a single pass. If you’re choosing a radius for a specific plywood thickness, our dedicated guide to rounding plywood edges breaks down the exact bit-radius-to-thickness match in more depth than fits here.
Flush-Trimming Plywood Edges with a Router
Flush trimming is a different job from cutting a sheet to size — it’s trimming an edge that’s already close to final size down to perfectly flush with a template, an existing surface, or an adjoining panel, and a router does it more precisely than a saw. A flush-trim or compression spiral bit rides a bearing along a template or straightedge and shaves the plywood edge exactly to that reference line. The compression geometry covered above is what keeps this specific cut clean on both faces, since a flush-trim pass typically removes only a small amount of material and any tear-out shows immediately on a cut that’s meant to be the finished edge.
This is a router-specific technique, not a substitute for cutting a full sheet down to rough size — if you’re breaking down a 4×8 sheet before it ever reaches this stage, that’s a saw job, and our guide to trimming plywood with a table saw or track saw covers blade selection and scoring for that separate step.
Router Speed and Feed Rate for Plywood
Smaller-diameter bits (up to about 1/2 inch) can run at the higher end of a router’s speed range, typically 18,000-24,000 RPM. Larger-diameter bits, including bigger round-over or panel-raising profiles, need to run slower — closer to 10,000-16,000 RPM — because the outer edge of a wide bit is moving much faster than a narrow one at the same RPM, and that extra surface speed is what burns the plywood’s glue lines instead of cutting cleanly through them. Feed rate should stay slow and steady rather than fast: a feed that’s too fast makes the bit take bigger bites than it can shear cleanly (more tear-out), while a feed that’s too slow lets the bit sit in one spot long enough to scorch the wood and glue line, especially visible as a dark streak along a cut edge.
Frequently Asked Questions
What Router Bit Should You Use on Plywood?
A downcut spiral or compression spiral carbide bit, not a straight or upcut bit. An upcut bit lifts the top-face veneer as it exits, which is the single most common cause of chip-out on plywood. A downcut bit pushes fibers down into the panel instead, and a compression bit (downcut on top, upcut near the bottom) cleans both faces at once, which matters most on dado and flush-trim cuts where both surfaces stay visible.
How Do You Router Plywood Without Splintering It?
Use a sharp downcut or compression spiral bit, run the cut as a conventional feed (the bit rotation pulls into the material rather than away from it), and clamp a scrap backer board flush against the exit side of the cut so the veneer has something to bear against as the bit passes through. Take the cut in two or three shallow passes instead of one deep pass, and always test on an offcut of the same sheet first, since veneer thickness and layer count vary between plywood grades.
Can You Cut a Dado Groove in Plywood With a Router?
Yes. A downcut spiral bit paired with a straightedge or router edge guide cuts a clean dado groove in plywood, and running it in two shallow passes rather than one full-depth pass keeps the top veneer from lifting. Support the panel fully underneath the groove location, since plywood flexes more than solid stock at the same thickness.
Can a Router Cut Through 3/4-Inch Plywood in One Pass?
It can, but it shouldn’t on a chip-out-prone cut like a dado or a full edge profile. Most 3/4-inch plywood actually measures closer to 23/32 inch, so set the bit depth off a direct caliper measurement rather than the nominal 3/4-inch spec. For dado and groove cuts specifically, two to three shallower passes give a cleaner result than forcing the full depth in one pass.
Bottom Line
Plywood routers just as cleanly as solid wood once you swap in a downcut or compression spiral bit, feed with a conventional pass, and back up the exit side of the cut. The panel isn’t the obstacle — matching the bit to how plywood is actually layered is.
Sponsored / affiliate links. As an Amazon Associate I earn from qualifying purchases. I may earn additional commission from eligible campaigns.